FL-GW-SS
Steel Shell Induction Melting Furnace
Fully welded steel-shell furnace with magnetic yoke and hydraulic 95° tilting, from 0.5 to 5 tons per body — the standard choice for continuous foundry melting.
Read More →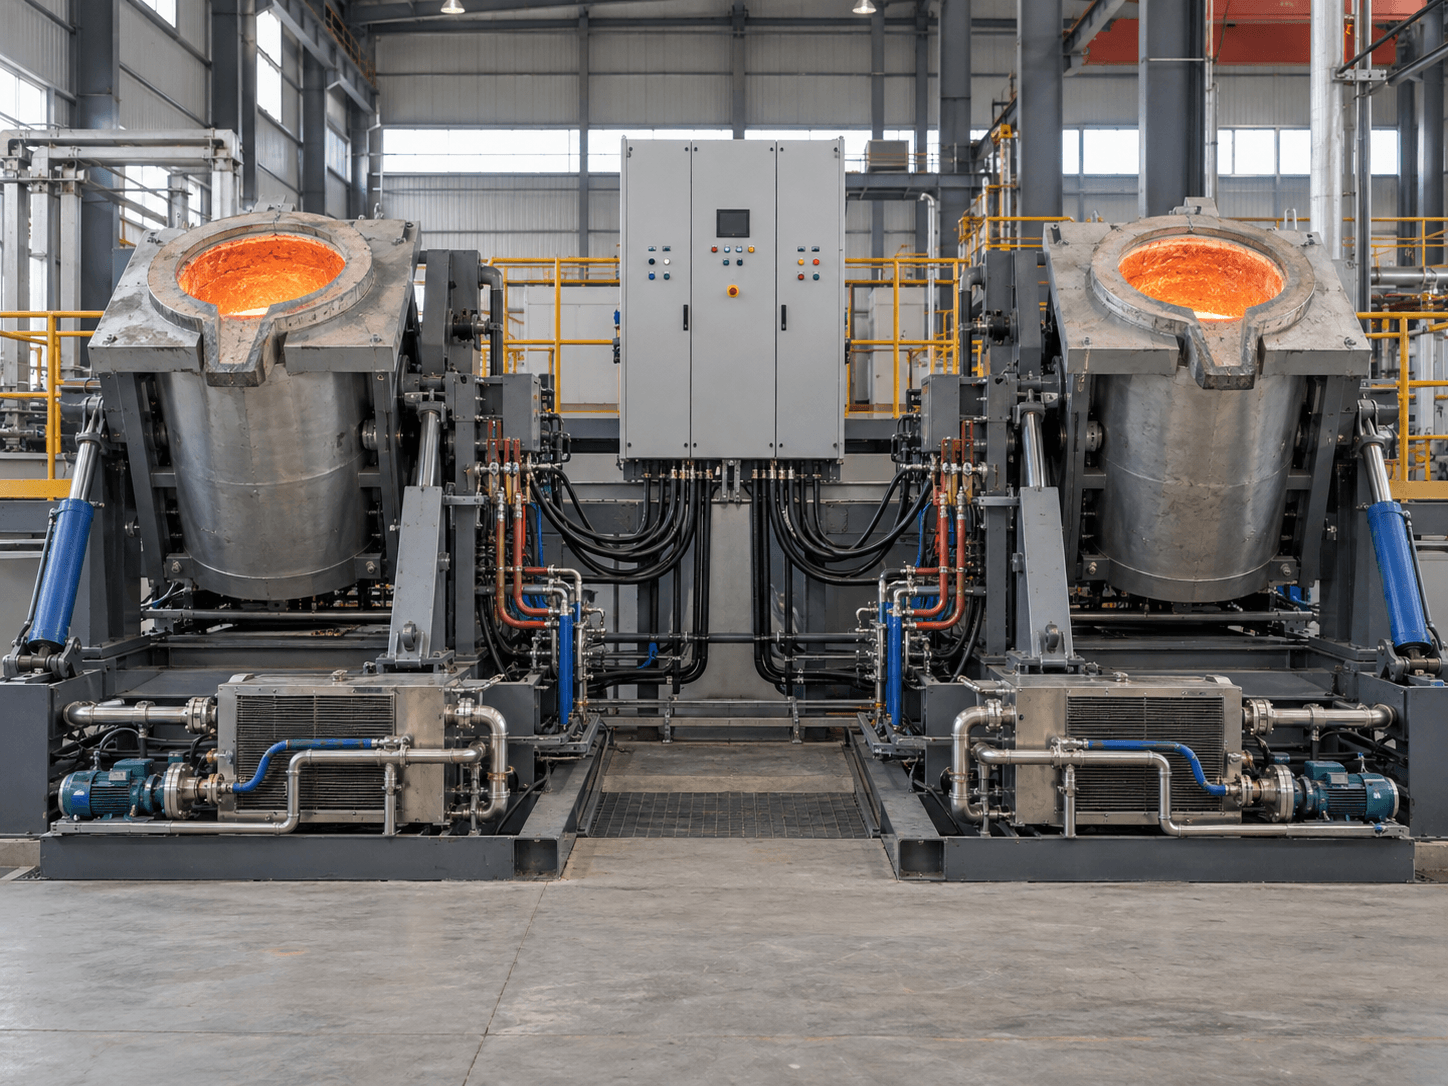
Induction heating manufacturer since 1998 · Built to your grid voltage · Installation & commissioning worldwide
Melting Furnaces · FL-GW-AS
Lightweight aluminium-frame furnace for small and medium foundries — lower installed cost, faster relining, ideal below 3 tons.
Standard models below. Capacity, power and frequency are matched to your alloy, output and grid at the quotation stage — non-standard ratings are built to order.
| Model | Capacity | Rated power | Frequency | Melting rate (steel) |
|---|---|---|---|---|
| GW-0.1 | 100 kg | 100 kW | 2,500 Hz | 0.12 t / h |
| GW-0.15 | 150 kg | 160 kW | 2,500 Hz | 0.18 t / h |
| GW-0.25 | 250 kg | 200 kW | 1,000 Hz | 0.25 t / h |
| GW-0.5A | 500 kg | 350 kW | 1,000 Hz | 0.45 t / h |
| GW-1A | 1 t | 700 kW | 500 Hz | 0.9 t / h |
| GW-2A | 2 t | 1,000 kW | 500 Hz | 1.4 t / h |
| GW-3A | 3 t | 1,500 kW | 350 Hz | 2.0 t / h |
Technical values require confirmation against the final equipment configuration. Aluminium-shell construction is recommended up to 3 t and for single- or two-shift duty. For continuous three-shift melting above 1 t, specify the steel-shell version.
The aluminium-shell furnace uses a thickened cast aluminium alloy frame instead of a welded steel structure with yokes, wound with thick-wall copper coil. It is lighter, cheaper to ship, and quicker to reline, which makes it the economical choice for job foundries and workshops melting below three tons per heat.
The body uses an open-bottom design with cooling rings at the base of the coil. Keeping the bottom of the lining cooler is what extends refractory life on a furnace that has no magnetic yoke to carry heat away from the coil.
Because there is no magnetic yoke, the design is best suited to intermittent or single-shift duty rather than continuous three-shift melting. Where a customer runs continuously above 1 ton we normally recommend the steel-shell version instead, and we will say so before quoting.
Supplied complete with power supply, capacitor cabinet, water-cooled cable, hydraulic or manual tilting, cooling system and control desk.
FL-GW-SS
Fully welded steel-shell furnace with magnetic yoke and hydraulic 95° tilting, from 0.5 to 5 tons per body — the standard choice for continuous foundry melting.
Read More →FL-GW-DT
Two furnace bodies sharing a single medium frequency power supply, switched from one console so melting never stops for a lining change.
Read More →FL-GWL
Low-frequency induction furnace tuned for aluminium and its alloys, with gentle stirring, low burn-off and a holding mode for die-casting lines.
Read More →FL-GWT
Medium frequency furnace for copper, brass and bronze with zinc-vapour extraction and tilting pour, sized 100 kg to 10 tons.
Read More →Send your alloy, target output per hour, working hours and grid voltage. You will get a capacity recommendation, a plant layout and a firm quotation — normally within three working days, no obligation.